Follow Us


Copyright MHI © 2026 | All Rights Reserved
Rapid growth and increasing customer expectations are placing ever greater demands on third-party logistics (3PL) providers to deliver speed, accuracy, and full traceability. At U.S.-based Commonwealth Warehouse Inc., the transition from paper-based processes to digital data capture using KEYENCE BT Series handheld computers is driving dramatic improvements in accuracy, throughput, and QA process management.With its headquarters in St. Bernard, Ohio, Commonwealth Warehouse operates a total of seven facilities in Ohio and Kentucky, primarily around the Cincinnati area.“We provide 3PL support through flexible warehousing space, multimodal transportation, and fulfillment,” explains Tom Hull, the company’s QA Manager.From paper to precisionAs the business scales, so too does the need for more robust quality control and traceability. Previously reliant on manual, paper-based systems, Commonwealth Warehouse faced inherent limita“Prior to adopting KEYENCE handheld computers, we relied on paper pick tickets and paper receipts,” says Hull. “The potential for human error was clear, and it would inevitably cause issues from time-to-time. We require full traceability on any license plate - pallet, container, box - moving through our system. It’s essential to have complete confidence in item and lot number accuracy, especially in the event of a client recall, where an immediate response is paramount.”To address these challenges, Commonwealth Warehouse implemented a fleet of KEYENCE BT Series handheld computers, primarily the BT-A700 model, alongside a smaller number of BT-A600 devices for a specialized application.Seamless integration, immediate impactA key factor in the success of the project was seamless integration between the KEYENCE devices and the company’s new warehouse management system (WMS): Synapse WebRF by Made4Net.“It was virtually plug and play; so simple and smooth,” reveals Hull. “Setting up one BT Series handheld computer took about five minutes before we cloned the configuration across the rest. If we received a batch of devices in the morning, they would be delivered to work locations and operational by lunchtime.”“We kept hearing from existing users of our chosen WMS that the KEYENCE BT Series was what we needed, and that’s proven absolutely correct,” he adds.Driving accuracy and eliminating errorsThe transition to digital scanning has delivered immediate and measurable benefits, particularly in reducing costly mis-shipments.“I estimate we’ve saved thousands of dollars just by eliminating mis-shipments caused by human error,” says Hull. “Accuracy is the biggest improvement.”The BT-A700 handheld computers, which make up most of the company’s deployment, offer a wide reading range, from just a few centimeters up to 10 meters, enabling operators to scan items quickly and reliably.Their ergonomic design and robust wireless connectivity further enhance productivity in busy warehouse environments.Meanwhile, the BT-A600 models play a critical role in a specialized customer project at Commonwealth Warehouse that requires validation between two labels on outbound shipments.“The BT-A600 is vital for that application,” explains Hull. “We need to confirm that specific fields on two labels match before shipping. The accuracy and speed of the BT-A600 scanners make it possible.”By leveraging the BT Application Design Tool in combination with AI powered OCR (optical character recognition), the device can capture barcodes, read printed text, compare required data points between both labels, and record each verification. Together, these capabilities deliver precise and dependable label validation beyond the limits of traditional barcode scanning technology.Transforming receiving operationsOne of the most significant operational improvements is in the receiving process, where digital data capture has dramatically reduced dock-to-stock times.“If the product is properly labeled, we can scan it as we unload the truck and it becomes available in the system immediately,” says Hull. “Previously, we had to write everything down, label it, put it away, and then manually enter the data. Dock-to-stock could take 90 to 120 minutes, sometimes longer for bulky items. Now we can process a full truckload in as little as 15 minutes in some cases.”Enhancing QA and visibilityBeyond speed and accuracy, the KEYENCE BT Series devices are strengthening Commonwealth Warehouse’s QA management processes.“Auditing used to be a long process,” he remarks. “Auditors would pick pallets, write down information, and then return to the office for verification against the system. Now they just scan the pallet, and the system tells them exactly what should be there. The auditors compare it physically and the job is done.”The ability to scan items anywhere in the workflow, including on trucks or in staging areas, ensures real-time visibility across operations, providing “a huge advantage”.Flexible, future-ready technologyAnother important benefit is the flexibility offered by the KEYENCE development environment, facilitated by the BT Application Design Tool.“We’ve been able to develop custom applications to support specific customer requirements,” says Hull. “If the scope of a project changes, we can adapt quickly. That’s been huge for us and provides opportunities for future projects as well.”The ability to manage multiple data formats, including barcodes, QR codes, and OCR (Optical Character Recognition), further supports the diverse needs of Commonwealth Warehouse’s customer base.Strong partnership and ongoing supportHull is equally positive about the company’s experience of working with KEYENCE.“Fantastic - one of the best suppliers I work with today,” he says. “KEYENCE have been very supportive and responsive, from initial selection through to on-site support and aftersales service.”He concludes: “It’s clear to see that we’re not shy about investing in quality. If there’s a way to improve accuracy and customer satisfaction, we’ll do it. Our investment in KEYENCE handheld computers exemplifies that ethos.”About KEYENCEKEYENCE has steadily grown since 1974 to become an innovative leader in the development and manufacturing of automation equipment worldwide. Our products consist of automation sensors, static eliminators, barcode readers, measuring instruments, vision systems, laser markers, and digital microscopes.ContactBrenna RotiPhone: (201) 930-0100 ext.70605Brenna.Roti@keyence.com
Trumann, AR - Roach Conveyors has received U.S. Patent No. 12,722,904 B1 for its CrossX™ Easy Transfer Roller, a conveyor roller design that converts a standard roller conveyor section into a bidirectional lateral transfer surface without requiring modifications to the existing conveyor frame.CrossX™ replaces standard 1.9-inch O.D. grooved conveyor rollers and allows cartons, totes, and irregular loads to move both along and across the conveyor surface. The design provides lateral movement and product reorientation using the existing conveyor frame, providing an alternative to replacing the section with a transverse roller top belt conveyor.Designed as a drop-in roller replacement for compatible 1.9-inch O.D. grooved conveyor frames, CrossX™ allows facilities to upgrade an existing conveyor section by changing the rollers while retaining the existing frame.CrossX™ also addresses ergonomic challenges in parcel, distribution, and manufacturing applications where operators manually move products across conveyor lines. Testing showed that CrossX™ can reduce the push force required to move a load by up to 80 percent compared to standard conveyor rollers.Applications include manual transfer zones, right-angle transitions, sorter support areas, intersecting conveyor lines, ergonomic workstations, and other operations requiring controlled lateral movement.CrossX™ is available in configurations for gravity, grooved, Poly-V, belt-driven live roller, and chain-driven live roller conveyor applications.For more information about the CrossX™ Easy Transfer Roller, visit roachconveyors.com/crossx or contact Roach Conveyors.About Roach ConveyorsFounded in 1953, Roach Conveyors manufactures conveyor systems and components for material handling applications across parcel and e-commerce, warehousing and distribution, manufacturing, packaging, airports, and other industries. Roach designs and manufactures conveyor equipment at its facility in Trumann, Arkansas, with solutions ranging from standard conveyor products to custom systems engineered around specific application requirements.
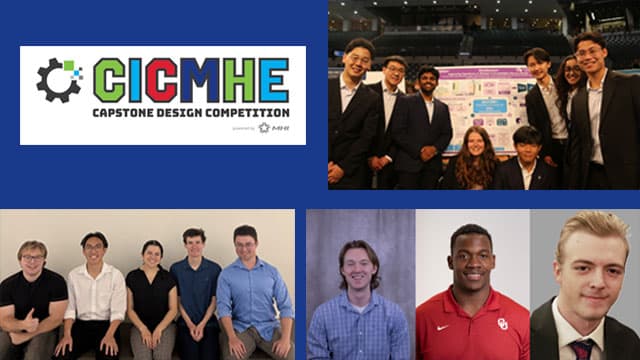
MHI & CICMHE are proud to recognize the winners of the 2025-2026 Material Handling Capstone Design Competition. The competition celebrates innovative material handling solutions while fostering student interest in the material handling industry as a rewarding career path.For the 2025-2026 competition, six different schools submitted a combined total of 11 entries. The submissions were evaluated by a set of industry and academic judges based on: Project complexity and outcome success Creativity in addressing the problem Potential impact/contribution to the material handling industry Quality of the deliverables Effective communication of the problem, approach, design, and resultsWe are pleased to announce the following winners:First Place Winner ($3,000) Georgia Tech & Wellstar Health System: Improving Operations at Wellstar’s Consolidated Service Center Student Team Members: Junwon Min, Eric Baw, Sujan Ganesh Kumar, MacKenzie Hulsey, Nano Suresettakul, Aron Cheng, Alka Rao, and Patrick Tangente Faculty Advisors: Drs. Gunter Sharp and Ying Laura LiSecond Place Winner ($2,000) California Polytechnic State University, San Luis Obispo & Cal Poly Microfabrication Laboratory: Cal Poly Microfabrication Laboratory Facility Layout Redesign Student Team Members: Finnegan Wallace, Darin Gong, Leah Perez, Cooper Hayashi, and Logan Bell Faculty Advisor: Dr. Mohamed AwwadThird Place Winner ($1,000) University of Oklahoma & BOSCH: Dynamic Nesting Value Stream Evaluation Student Team Members: Kaden Holt, Ralford Mullings, and Lucas Edwards Faculty Advisors: Drs. Byeong-Min Rob and Doyle DoddThanks to the generous MHI sponsors for the 2025-2026 competition, including the MHI Solutions Community, Swisslog, KNAPP, Proactive Global, and Fives Intralogistics Corp, who made the award money possible. Additionally, we would like to thank the following individuals for serving on the judging panel: Naveen Chandra Kukkala (EssilorLuxottica), Steve Hopper (Inviscid Consulting), Jason Looman (Scanreco), Derek Westfall (Westfall), Glen Wegel (Kitchen Cabinet Distributors), Prabhat Rao Pinnaka (Lowe’s), Joshua Joseph (Tesla), and Mary Beth Kurz (Clemson University).Congratulations to all the winning teams, their industry clients, and their faculty advisors. To learn more about the competition, please visit mhi.org/cicmhe/capstone-design-competition.About MHIMHI is an international trade association that has represented the material handling, logistics and supply chain industry since 1945. MHI’s over 1,000 members include material handling and logistics equipment and systems manufacturers, integrators, consultants, workforce solution providers, publishers and third-party logistics providers. MHI offers education, networking and solution sourcing for their members, the members’ customers, and the industry as a whole through programming and events. The association produces the ProMat and MODEX expositions that showcase the products and services of its member companies to educate manufacturing and supply chain professionals. The Warehousing Education and Research Council (WERC) is a division of MHI and provides education and research to the warehousing, distribution, and logistics community.
Company adds nearly 130,000 square feet of manufacturing and office space as workforce grows by more than 200 employeesBLAIRSVILLE, Ga. — Panel Built, Inc., a leading manufacturer of custom modular buildings and steel structures, is significantly increasing its production capabilities following strong company growth.Over the past year, Panel Built has hired more than 200 employees while investing in nearly 130,000 square feet of new and expanded office and fabrication space. The projects include major additions to two of the company's Georgia locations, as well as a 50,000-square-foot plant in Etowah, Tennessee.In Georgia, construction is well underway on a 73,000-square-foot expansion of Panel Built's Blairsville headquarters. The new modular addition will provide the office and manufacturing space needed to accommodate increased production demands and a larger workforce. Construction is expected to be completed later this year.Panel Built is also adding 6,400 square feet to its Blairsville welding facility, providing additional room to take on larger, more complex projects for the utility industry and other customers.Beyond Georgia, Panel Built has increased its presence in Tennessee, recently opening a second location in McMinn County. The new 50,000-square-foot Etowah plant supports Panel Built's steel fabrication work and is equipped with new laser cutting equipment, an automated beam line, and powder coating operations. The company chose to invest further in Etowah after the success of its first location there, which opened in 2024.For these expansions, Panel Built has been able to draw on its own engineering, manufacturing, and modular construction expertise. Much of the work has been implemented by Panel Built's own teams, ensuring the projects move quickly and allowing production to continue during construction.Michelle Murray, Panel Built's HR Manager, credits the company's employees with making the recent expansion possible.“It’s been exciting to see how much we’ve grown over the past year,” said Murray. “We’ve welcomed more than 200 new employees, and at the same time, we’ve watched these new spaces take shape around us. Our team has put a lot of hard work into getting Panel Built to this point, so it’s rewarding to see that growth happening firsthand.”Together, these investments strengthen Panel Built's presence in the Southeast and its ability to meet rising customer demand. With its newest Tennessee plant now operational and construction on the Blairsville additions moving toward completion, the company continues its commitment to the future of American manufacturing.About Panel Built, Inc.Founded in 1995, Panel Built, Inc. designs and manufactures custom modular offices, mezzanines, cleanrooms, security buildings, e-houses, and other prefabricated structures for customers throughout North America. With production facilities in Georgia and Tennessee, Panel Built provides custom American made space solutions designed around the needs of each customer.